
Biomass Conversion Pilot Plant
NLR's Biomass Conversion Pilot Plant enables researchers, industry partners, and stakeholders to test a variety of integrated, performance-enhanced chemical conversion processes and technologies.

NLR's 27,000-ft2 high-bay Biomass Conversion Pilot Plant accommodates bench-to-pilot-scale processes for converting cellulosic biomass into a variety of chemicals and fuels at process throughputs of up to 1 tonne of dry biomass per day.
Experiments in the Biomass Conversion Pilot Plant are supported by NLR's technological scale-up and piloting research. NLR's analysis, characterization, modeling, and super intelligence research helps accelerate the translation of laboratory-scale conversion pathways to commercial-scale production.
Revitalization Effort
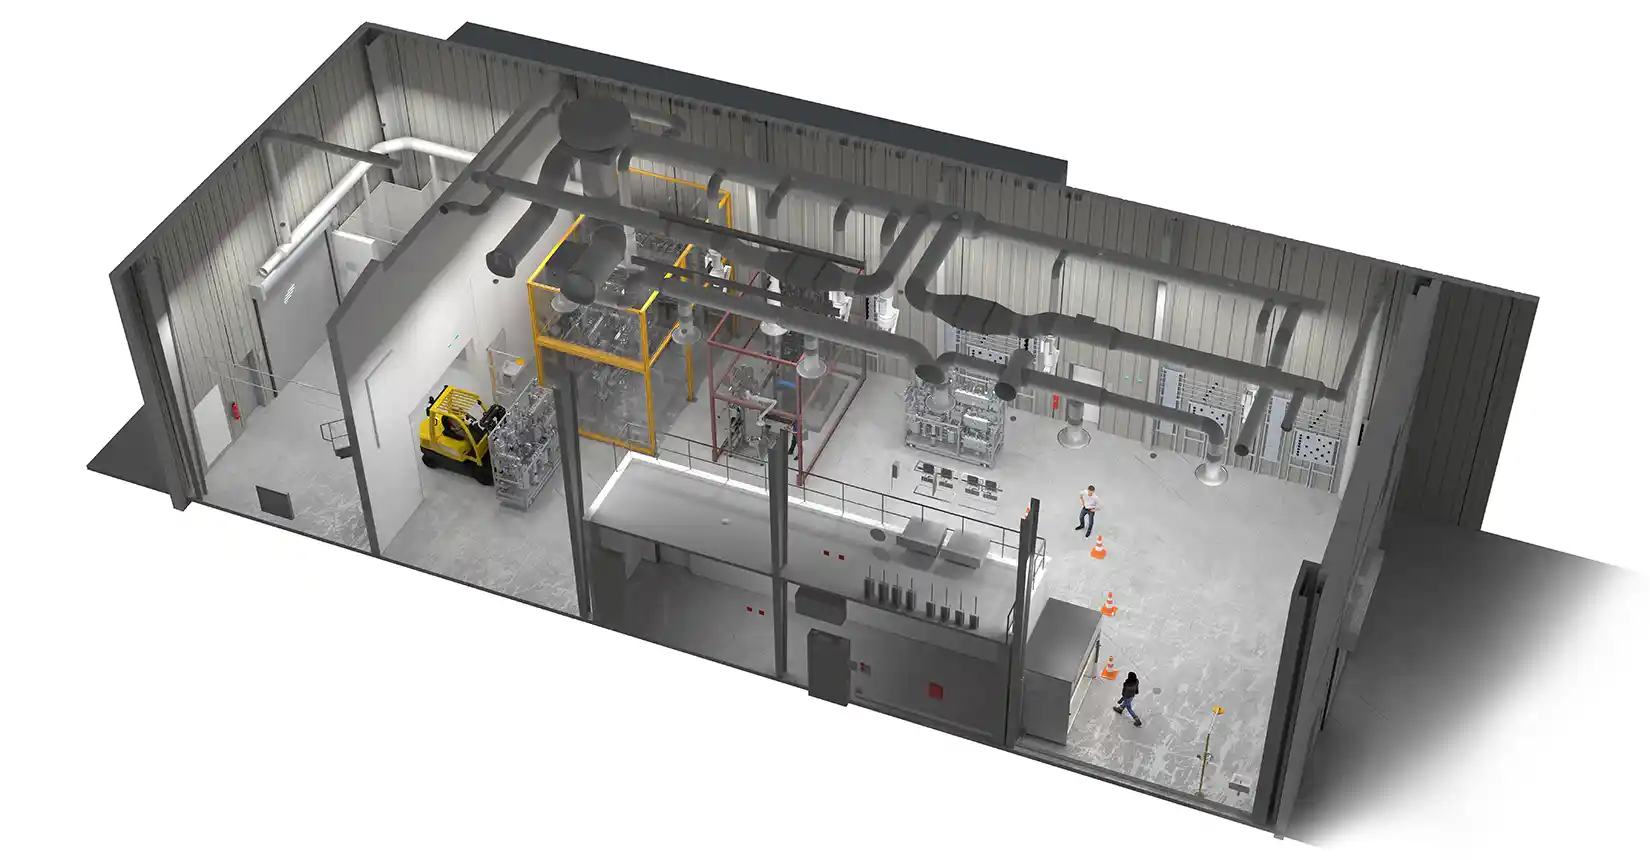
Since its design and construction in the mid-1990s, NLR's Integrated Biorefinery Research Facility has been a significant asset to the U.S. Department of Energy in building valuable R&D partnerships across the bioeconomy. Now, to meet the challenges of developing the next generation of chemical, fertilizer, and critical mineral technologies, NLR is modernizing the facility.
Key upgrades to the Biomass Conversion Pilot Plant enable cost-effective, timely, and technically rigorous piloting by using:
Plug-and-play modular concepts for rapid reconfiguration and integration of new and existing equipment to reduce costs
Full process integration from feedstock to finished products at Technology Readiness Level 5/6, incorporating biochemical, thermochemical, and electrochemical equipment
Rigorous analytics and data tracking using highly instrumented systems to allow for deep understanding of process
Comprehensive modeling—including digital twin, computational fluid dynamics and techno-economic and process analysis—to accurately simulate and derisk technologies
Scale-up support with experienced and dedicated personnel to ensure high-integrity data and that lessons gained are scalable
House equipment and utilities to minimize technology scale-up barriers, enabling a quicker path to commercialization.
Together, these enhancements significantly boost the facility's flexibility, speed, safety, scale-up, and piloting capabilities. These capabilities will accommodate biochemical, thermochemical, and electrochemical research from bench-scale to pilot-scale for decades to come.
Core Capabilities
NLR's Biomass Conversion Pilot Plant has these capabilities:
Storage area for feedstock delivered in totes, drums, or supersacks
Mobile knife mill for smaller sample preparations
Pulp fibrillation instrument mill for batch pulping
Capacity: 20–40 g (dry basis)
Two knife milling systems with dust collection
Capacity: 100 kg/hour (dry basis)
Mobile 12-in. disc refiner with manual plate gap adjustment at 0.025-mm increments
Mobile planetary ring-roller mill for wet and dry grinding
Feed surge hoppers and pneumatic conveyance to pretreatment systems
Cyclones for milled product collection
Batch reactors
-
4-L steam-explosion batch reactor
-
Maximum temperature: 238°C
-
Saturated steam pressure: 450 pounds per square inch gauge (psig)
-
Construction: Hastelloy C-22
-
-
90-L batch paddle-type mixed reactor
-
Construction: Alloy 20
-
Maximum allowable working pressure (MAWP): 90 psig
-
-
170-L batch paddle-type mixed reactor
-
Construction: Hastelloy C-22
-
MAWP: 350 psig
-
-
All reactor systems have multiple options for pretreatment catalysts
Continuous reactors
-
Continuous horizontal screw-type reactor system
-
Four auger reactors in series
-
Capacity: 0.5 tonnes per 24-hour day of dry biomass
-
Operating temperature: 140°–210°C
-
Residence times: 3–120 minutes
-
Construction: 316 stainless steel and Hastelloy C-2000
-
-
Continuous vertical reactor
-
Inline secondary reactor for optional treatment at lower temperatures
-
Capacity: 0.5–1 tonne per 24-hour day of dry biomass
-
Operating temperature: 140°C–210°C
-
Residence times: 2–60 minutes
-
Construction: 316 stainless steel and Hastelloy C-2000
-
-
All reactor systems have multiple options for pretreatment catalysts
Reactors
30-L batch or continuous paddle-type mixed reactor
Construction: 316 stainless steel
MAWP: 100 psig
1,900-L batch paddle-type mixed reactor with hot-water jacket
Construction: 316 stainless steel
MAWP: 50 psig
Four 4,000-L semicontinuous processing paddle-type mixed reactors with hot-water jackets
Total solids loadings greater than 20% (w/w)
Construction: 304 stainless steel
Pilot plant bioreactors
Two 160-L fermentation vessels
Two 1,500-L fermentation vessels
Four 9,000-L fermentation vessels
Capabilities
All systems can be run independently or sequentially
Operation modes: batch, fed-batch, or continuous
Fully instrumented to control pressure, temperature, pH, weight (level), and dissolved oxygen
Off-gas monitoring with mass spectrometry
Aerobic or anaerobic operation
Agitated (two impellers per tank) and aerated
Clean-in-place installation
Continuous high-temperature, short-residence-time sterilizer
Construction: 316 stainless steel
MAWP: 50 psig to full vacuum
Centrifugation
120-L bowl perforated basket filtering centrifuge
Construction: Hastelloy
Speed: 900 gravitational force
320-L bowl perforated basket filtering centrifuge
Construction: 316 stainless steel
Speed: 900 gravitational force
Disc stack centrifuge
Typically used for microbial cell separation
Continuous operation capable of both two-phase or three-phase separations
Construction: 316 stainless steel
Speed: 11,000 gravitational force
Horizontal solid bowl centrifuge
Designed for continuous high-g force separation of industrial slurries into liquid and solid phases
Construction: 304 stainless steel
Other systems
Tangential-flow (cross-flow) filtration
Currently configured for microfiltration
Circulation rate: 18,000 L/hr
Permeate rate: 1–3 L/min (depending on feed characteristics)
Construction: 316 stainless steel
Forced circulation evaporator
Continuous feed capabilities
Handling insoluble solids up to 5 wt% biomass
Water evaporation rate: 500 lb/hr
Construction: 304 stainless steel
MAWP: 75 psig
Bench- and pilot-scale biomass chemical impregnation and dewatering systems (screw presses)
Research in the Biomass Conversion Pilot Plant taps into NLR's suite of special-purpose laboratories, including:
Compositional analysis
Process engineering and economic analysis
Molecular biology
Microscopy analysis
Rheology and particle size characterization
High-throughput processing and analysis
Computational modeling.
Contact
Work With Us
Learn how to work with NLR to develop, translate, and de-risk bioeconomy innovations for market readiness.
Share

Last Updated Oct. 22, 2026